Custom cable projects often go over budget or miss deadlines due to pre-design-freeze decisions that look technical but are commercial. This article examines the decisions that really matter—conductor stranding, insulation thickness, certification, ampacity correction, batch consistency, and cost structure and why they are so often underestimated.
Conductor Stranding: A Complex Problem That Gets Oversimplified
1. Lay Length and Direction
“Class 5 is for mobile applications, Class 6 is for high-frequency bending” is not wrong but far from enough. Bending life depends mainly on three parameters: lay length, stranding direction, and individual wire diameter. Shorter lay length improves flexibility but raises manufacturing cost. If stranding runs in the same direction as cabling, the cable twists as a whole when bent, adding stress to the shield and jacket.
For reel equipment, shortening lay length from 12 times the outer diameter to 8 times can raise bending life from tens of thousands of cycles to hundreds of thousands in some bending tests, but conductor cost rises noticeably. That trade-off is rarely discussed in many projects.
2. Wire Diameter and Conductor Material
Individual wire diameter matters too. For the same cross-section, finer wires improve flexibility but add drawing and stranding passes, raising cost. Class 6 typically uses finer wires than Class 5, and bending life can differ several times. Every stranding adjustment trades flexibility against cost and manufacturability.
Conductor material is a separate decision. Copper remains the default, with the highest conductivity and good mechanical strength. Aluminum is lighter and cheaper but needs a larger cross-section for the same ampacity. Copper-clad aluminum balances cost and connectivity, while tinned copper suits moisture or chemical exposure.
3. Why “Class 5” Is Not Enough
The problem is that many buyers work with general requirements like “Class 5” rather than specific application conditions. If the manufacturer simply follows the words without asking about actual bending frequency and bending radius, the final product may be neither economical nor durable.
Once the conductor is settled, the next design decision is insulation. It looks simpler than the conductor, but the traps often run deeper.
Insulation Thickness: Safety Margin Is Not Waste
1. How Much Does Thinner Insulation Really Save?
“Thinner insulation can reduce cost” is technically true, but commercially it is often a trap.
Insulation thickness is designed based on voltage class and mechanical strength requirements. For a 0.6/1 kV PVC-insulated cable, standard insulation thickness is roughly between 0.7 mm and 1.0 mm, depending on conductor cross-section. If insulation thickness is reduced by 20 percent, the amount of insulation material itself can be cut by about 20 percent, but the reduction in total cable cost is usually only a few percentage points—because insulation compound accounts for a much smaller share of total cost than the conductor.
The price is a simultaneous drop in both electrical margin and mechanical abrasion resistance.
2. Voltage Fluctuation and Mechanical Damage
The problem is that in many applications, voltage is not stable. Voltage fluctuations in industrial power grids, harmonics, and transient overvoltages can all make actual insulation stress higher than the nominal value. If insulation thickness is designed at the lower limit of the standard, these extra stresses will accelerate insulation aging.
The most hidden problem is mechanical strength. During installation and operation, the insulation layer must withstand bending, pulling, and friction. Thinner insulation is more likely to be damaged during construction, and the damage often does not show up immediately—it appears months later as an insulation failure.
3. Material Choice Sets Performance Limits
Insulation material choice is equally critical. PVC covers 70°C at low cost. XLPE offers good dielectric properties and short-circuit tolerance to 250°C. EPR suits mobile and vibrating use. LSZH serves public and confined spaces. Silicone handles extreme temperatures. For jackets, PVC is abrasion- and oil-resistant; PE handles outdoor weather; TPU suits drag chains and reels; chloroprene serves industrial environments.
Insulation thickness cannot be based on voltage class alone. Installation conditions, operating environment, and expected life all matter. For long-life, high-reliability projects, sufficient margin is risk control, not waste.
Once the design is frozen, the next question is how to prove the cable meets target-market requirements. That leads to certification, whose path often affects scheduling more than expected.
Certification Path: More Easily Underestimated Than Testing
1. CB Scheme: What It Saves and What It Doesn’t
Multi-country export projects often use the CB scheme. CB test certificates and CB test reports can be converted among IECEE member countries, reducing duplicate testing. That sounds good, but in practice there are several key limitations, and these limitations directly affect project scheduling.
CB covers IEC standards, but national differences still require separate evaluation—converting to UL, for example, needs extra U.S. tests like UL 83 for THHN. Lead time is not short; the “quick swap” idea is a myth. Validity also depends on the issuing NCB, whose acceptance varies by country and affects conversion difficulty.
2. Certification Fragmentation Across Markets
Fragmentation is accelerating. In North America, UL standards such as UL 44, UL 83, and UL 854 continue to tighten, with more detailed and stricter test items than a few years ago. In Europe, CPR certification is moving toward finer classification, with smoke production and flaming droplet requirements far stricter than ordinary flame-retardant cables.
In India, BIS certification for cables has been mandatory for many years—not “moving from voluntary to mandatory”—and it requires factory audits and ongoing surveillance. In the Middle East, Saudi Arabia requires export goods to obtain a certificate through the certification system before arrival; applications after arrival are considered invalid. Certification is shifting from one-time testing to ongoing local compliance.
3. When to Apply Directly for Target-Market Certification
PV or marine cables may need direct target-market certification; CB has limited value. The key decision is route, time, and issue. Doing it at the design stage costs least; patching later multiplies rework.
Once the certification path is set, the cable enters selection and verification. Here a step that looks standard is often skipped: ampacity correction.
Ampacity Correction: Why Standard Tables Are Not Enough
1. The Assumptions Behind Standard Tables
Cable ampacity tables are usually based on specific conditions: ambient temperature of 30°C or 40°C, installation in air, a single cable, and no direct sunlight. Actual installation conditions almost never satisfy all these assumptions at the same time.
2. Derating for Bundling, Temperature, and Sunlight
Bundled cables dissipate heat poorly, so ampacity must be derated by bundle count, arrangement, and tray enclosure. The above-standard ambient temperature also needs correction: PVC cable at 40°C is roughly 10–15% lower than at 30°C; XLPE follows the same trend. Roof or sun-exposed trays add solar heat, raising conductor temperature 10–20°C above ambient and requiring further derating.
3. Who Does the Correction
These factors are in the standards, but many selections only check the ampacity table without applying them—leading to overheating, faster aging, or tripped protection. Correction belongs at the design stage, not after installation. It is skipped because it looks like table lookup, not a decision. Yet who does it, when, and under what conditions are decisions. If the buyer assumes the manufacturer handles it while the manufacturer assumes the buyer confirmed installation conditions, a gap appears.
Ampacity correction ensures stable operation under specific conditions. But even with correct design and selection, mass-produced cables must still match the sample—that is batch consistency.
Batch Consistency: A More Important Metric Than Sample Quality
1. A Good Sample Does Not Mean Good Production
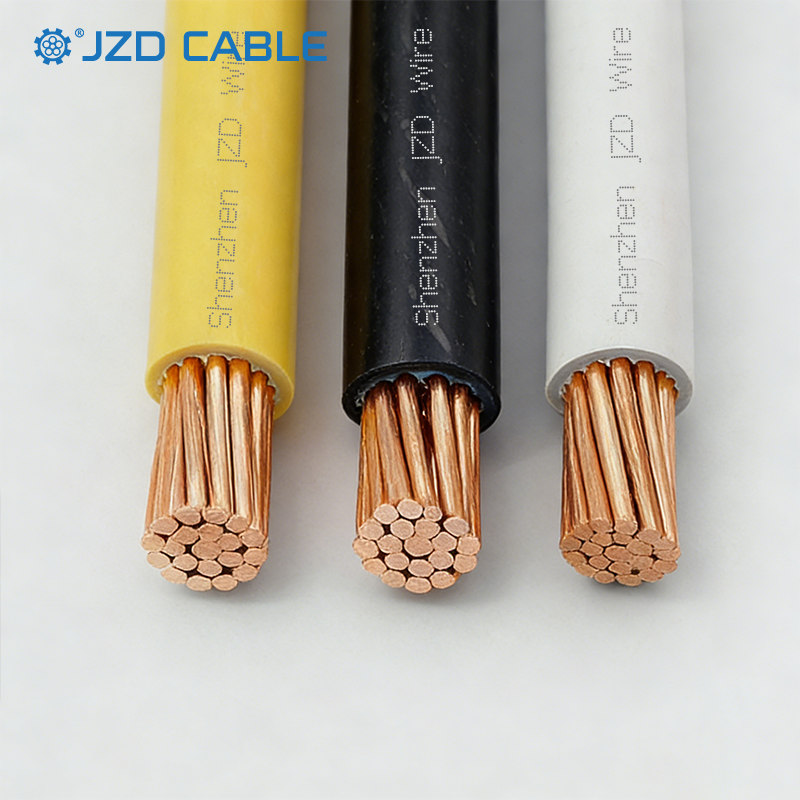
Samples are usually good because manufacturers know they’ll be inspected. The real test is mass production. Batch consistency depends on raw materials (copper conductivity, insulation formulation, plasticizer content), stable process parameters (extrusion temperature, pulling speed, lay length), and strict quality control (first-article, in-process, final inspection). For B2B buyers, repeat-order consistency matters more than first-sample quality: rework costs far exceed material price differences, and replacement after installation can cost several times the cable price.
2. How to Assess Consistency Capability
Check for statistical process control, complete batch records and traceability, regular internal and third-party audits, and historical complaint and return rates. Request this during supplier audits or verify through small trial orders—not to check sample quality, but to observe production consistency.
Batch consistency determines reliable delivery, but reliable delivery depends on cost. Back at the commercial level, let’s look at where the money goes and which cost decisions are easily misjudged.
Cost Structure: Where the Money Goes, That’s Where the Risk Is
1. Cost Composition
Custom cable cost typically covers raw materials, manufacturing, testing and certification, and packaging/logistics. Raw materials dominate, mostly the conductor.
2. Copper Price Terms
Copper volatility drives the need for a price baseline and adjustment mechanism—yet quote validity and adjustment terms are easily underestimated. Traditionally quotes last 30–60 days; with high volatility, suppliers may shorten validity or add copper clauses. Buyers who wait may face expired quotes or higher prices. Fixed-price contracts can backfire: suppliers may prioritize higher-margin orders when copper rises, delaying small custom batches.
3. Manufacturing, Testing/Certification, and Packaging
Manufacturing cost depends on process complexity and batch size; small batches amortize poorly, making custom cable costlier than standard. Testing and certification costs also amortize poorly in small batches—multi-country certification spread over a few hundred meters can sharply raise per-meter cost, so the certification path should be decided early. Packaging and logistics depend on coil length, reel type, and distance. Coil length looks like logistics but affects container loading and unit shipping cost by 10–20%.
4. Trade-offs in Cost Optimization
Cost optimization mainly lies in raw material selection and structural design. For example, replacing copper conductors with aluminum can significantly reduce cost but requires a larger cross-section and may affect installation space. Replacing XLPE with PVC can reduce cost, but the temperature rating drops and may limit ampacity. These trade-offs need to be evaluated for the specific application; there is no universal answer.
Final Thoughts
Back to the opening question: which decisions really affect cost and lead time, and why are they so easily underestimated?
The decisions are conductor stranding, insulation thickness, certification path, ampacity correction, batch consistency, and cost structure. Conductor and insulation specs are taken literally, not checked against real conditions. Certification is deferred as paperwork. Ampacity correction is mistaken for table lookup. Batch consistency is assumed from good samples. Cost structure omits copper volatility and certification amortization from quotation talks.
One takeaway: success is decided before design freezes. The most valuable work is not price haggling but clearly stating application conditions, certification targets, and installation environment so the manufacturer can flag what you missed. Contact us to discuss your project.